News

Industry News

WPC extrusion mould buying guide: from profile drawing to line acceptance15 2026-09

WPC extrusion mould buying guide: from profile drawing to line acceptance

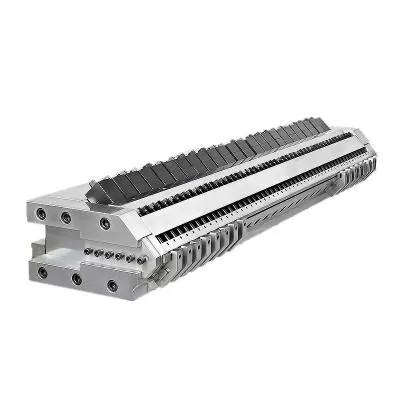
To buy a WPC extrusion mould, send the final cross-section with tolerances, the complete polymer and wood-filler formula, material preparation method, target output and line speed, extruder interface, downstream cooling layout and a finished-product acceptance plan. Mark visible surfaces, critical walls, internal ribs, cavities, radii and any embossing or sanding allowance on the drawing. Do not accept the tooling from a dry dimensional report alone. Run the agreed formula through the intended line, let the profile cool, then measure dimensions, wall and rib thickness, straightness, twist, surface condition and mass per length. Product performance tests remain the responsibility of the finished-product manufacturer.
Pipe extrusion die head buying guide: what to specify before you order15 2026-09

Pipe extrusion die head buying guide: what to specify before you order

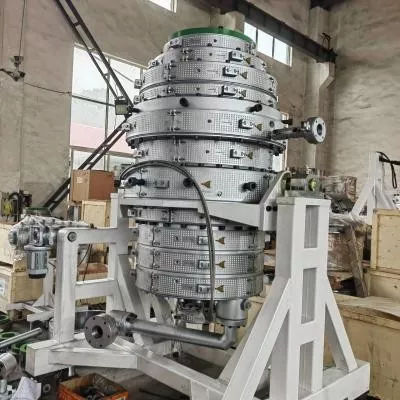
To buy a pipe extrusion die head, send the supplier five matched data sets: the material and formulation; the pipe standard, diameter and wall range; output and line speed; the extruder flange and melt-inlet interface; and the downstream calibrator, vacuum, cooling and haul-off arrangement. A request that gives only "PVC pipe, 110 mm" is not ready for engineering. The most important contract point is the acceptance condition. Name the actual production material, pipe size, stable output, line speed, heating and sensor setup, allowable wall variation, outside diameter, ovality, surface condition and required product tests. The die head shapes the hot melt, but it cannot by itself guarantee the final cooled pipe.
Parallel twin screw barrel clearance: what to measure before replacement15 2026-09

Parallel twin screw barrel clearance: what to measure before replacement

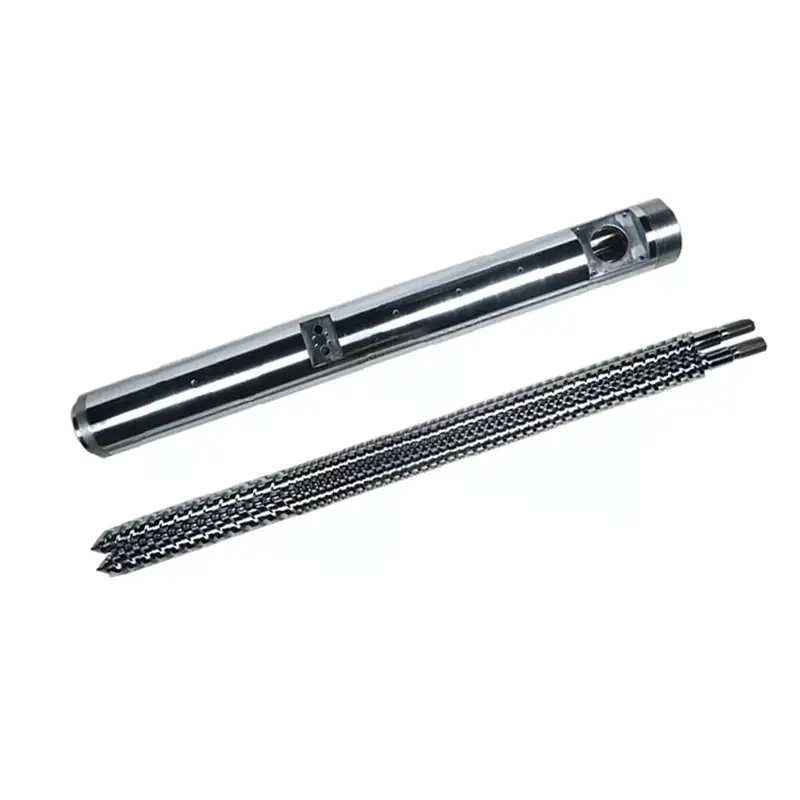
Measure parallel twin screw and barrel wear as a matched system. Record both screws at named axial stations, both lobes of the figure-eight bore in defined directions, screw-to-screw clearance, center distance, phasing and axial fit. Compare the map with the approved drawing. Symptoms can trigger inspection, but measurements decide whether to replace screws, barrel or the complete set.
How to specify a parallel twin screw barrel for high-filled PVC09 2026-09

How to specify a parallel twin screw barrel for high-filled PVC

For high-filled PVC, specify the complete recipe in phr, feeding method, end product, required output, screw rotation, center distance, connection dimensions and the wear map of both screws and barrel bores. Select nitriding, chrome plating or a bimetallic layer against the actual wear duty. Approve the drawing and inspection method before price becomes the deciding factor.
Injection molding screw recovery time too long? What to check before replacing the screw09 2026-09

Injection molding screw recovery time too long? What to check before replacing the screw

If injection molding screw recovery takes too long, first confirm that it delays the cycle. Then check feed continuity, actual screw speed, back pressure and temperature against a stable reference run. Inspect geometry and wear when those checks do not explain the loss. Replace components only after identifying the limiting function.
How to specify a conical twin screw barrel for PVC foam board09 2026-09

How to specify a conical twin screw barrel for PVC foam board

Choose a PVC foam board conical twin screw barrel around the formulation, the existing machine interfaces and the measured wear. Confirm the complete drawing before selecting a diameter pair. Specify nitriding or bimetal protection by production duty, then agree on an acceptance test using your actual board recipe and quality requirements.
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies. Privacy Policy
RejectAccept