News

Industry News

Single-screw vs parallel twin-screw pelletizing line: which one fits your material?09 2026-09

Single-screw vs parallel twin-screw pelletizing line: which one fits your material?

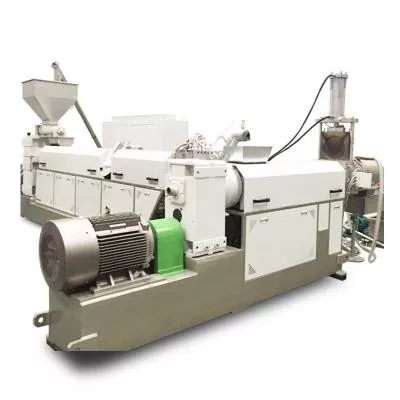
Choose a single-screw pelletizing line when the feedstock is already close to the final formulation and the main jobs are stable conveying, melting, melt filtration, pressure generation and pellet cutting. It is a practical starting point for consistent PE or PP regrind, simple re-pelletizing, laboratory work and small to medium production. Choose a parallel twin-screw pelletizing line when the machine must compound as well as pelletize. It is better suited to fillers, pigments, polymer blends, masterbatch, modified plastics, multiple feed streams and stronger devolatilization. Do not buy the twin-screw line only because its listed output is higher. Buy it when its process functions match the formulation.
Planetary screw vs single and twin screw: when is the upgrade worth it?31 2026-08

Planetary screw vs single and twin screw: when is the upgrade worth it?

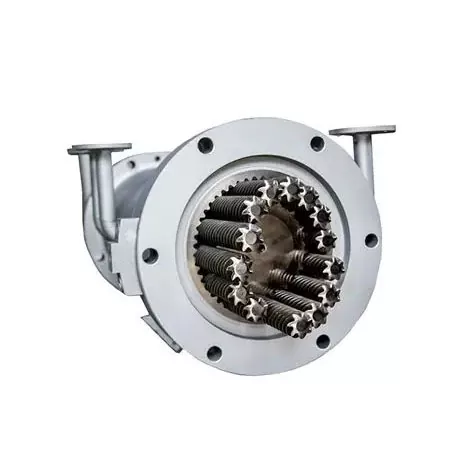
Choose a planetary screw when the formulation needs excellent distributive mixing, broad heat-transfer area, self-wiping action or staged degassing, especially with heat-sensitive PVC, high-filled compounds, elastomers, adhesives and composite materials. Stay with a single screw when the process is stable and mainly needs economical melting, conveying and pressure. Choose a co-rotating twin screw when high-speed compounding, flexible side feeding or stronger dispersive work is the priority. If the die needs more pressure than the planetary section can provide, plan the downstream pressure stage before ordering.
Injection molding screw tip selection: check ring wear, fit and RFQ checklist31 2026-08

Injection molding screw tip selection: check ring wear, fit and RFQ checklist

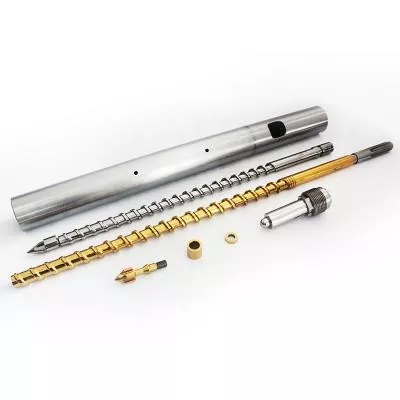
Choose an injection molding screw tip by four things: the non-return valve design, the exact screw and barrel interface, the processed resin and filler, and the wear pattern of the existing assembly. Machine model alone is not enough when versions, previous repairs or non-standard screws may exist. For a replacement order, send the original drawing when available, then verify the thread, shoulder, tip length, ring travel, seat, outside diameter and melt passages against the actual machine. A good quotation starts with geometry. Material and surface treatment come next.
Nitrided vs bimetallic single screws: match the surface to the resin and filler31 2026-08

Nitrided vs bimetallic single screws: match the surface to the resin and filler

Choose nitriding when a treated steel surface fits the verified wear, corrosion and dimensional duty. Choose flight hardfacing or another bimetallic construction when the project needs a different alloy in the highest-wear area. For severe service, the better answer may be a hardfaced screw with a compatible bimetallic barrel. No option is automatically superior. Start with the failure mode, then approve the screw and barrel materials, layer locations, processing route and inspection criteria together.
Screw speed, melt temperature and output: why one setting changes the others31 2026-08

Screw speed, melt temperature and output: why one setting changes the others

Increasing screw speed usually increases drag flow and the rate at which material enters the process, but the relationship is not unlimited or perfectly linear. More rpm can also add shear heat, shorten residence time and expose a weak feed or melting section. Change one controlled variable at a time, wait for a stable condition, then compare output, melt temperature profile, pressure, motor load and product quality. Stop when one of those reaches its approved limit, even if the drive can turn faster.
How to clean a single screw extruder without damaging the screw or barrel28 2026-08

How to clean a single screw extruder without damaging the screw or barrel

Use a layered method. Start with the material and machine supplier's approved purge procedure while the extruder remains under normal operating control. If residue returns or the screw must be exposed, stop, isolate and verify hazardous energy according to the plant procedure. For a removed screw, use component-approved non-damaging tools. Industry guidance recommends brass tools, copper gauze and cotton cloth, and warns against steel scrapers and localized torch heating. Inspect the clean surfaces before deciding that the problem is wear.
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies. Privacy Policy
RejectAccept